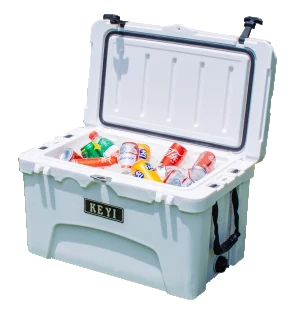
Commercial insulated containers
Define payload, temperature profile, openings and cleaning. Shell, foam, seal and closure affect insulation. Use a documented test rather than unsupported cooling days. Medical cold-chain and dry-ice use need separate validation.
What to send for a useful review
- Continuous, peak and minimum temperature
- Gaskets, connections and leak test method
- Cleaning agents, disinfection and access
- Target market, intended use and required evidence
- Test conditions and pass/fail limits
Catalogue examples show applications, not guaranteed specifications. Grade, dimensions, testing and delivery are agreed for each project.
Discuss your projectContinue exploring
Nominal vs minimum wall thickness
Nominal thickness describes a design target; minimum thickness defines the weakest acceptable inspected region. A part can meet its target weight and still have a thin local area. Agree a wall map around corners, fittings and highly loaded surfaces, with the measurement method and sampling plan. Increasing shot weight changes material cost and may lengthen the cycle, but does not automatically solve every thin spot. Check internal volume and mounting clearances when the wall changes.
Read guide ↗Why wall thickness varies
Wall distribution depends on heat, mold geometry, material movement and loading arrangement. Start with an inspection map and process records rather than accepting total weight as proof of uniformity. Investigate whether thin areas align with shielding, deep features or changes in powder movement. Trial one controlled adjustment at a time and verify the other surfaces have not become unacceptable. A uniform-looking exterior does not reveal the condition of the inside wall.
Read guide ↗Tolerances, shrinkage and assembly datums
Specify the few dimensions that actually control assembly and explain their function. A single tolerance percentage for every rotomolded part is not a useful acceptance standard. Separate molded envelope dimensions from machined interfaces and hole positions. Agree when the part is measured, its support condition and the reference datums. Test the sample on the real mating equipment. A tool made accurately does not remove the influence of resin, pigment and cooling on the final part.
Read guide ↗